Ferrous metals and their alloys (steel, iron, manganese, nickel, etc.) have high melting points, typically requiring 1500-1750°C melting temperatures, demanding exceptional temperature resistance, lining life, power density, and melting efficiency. Henan Rongke Electric delivers high-power medium-frequency melting solutions specifically designed for steel, iron, manganese, nickel and their alloys based on induction heating technology.
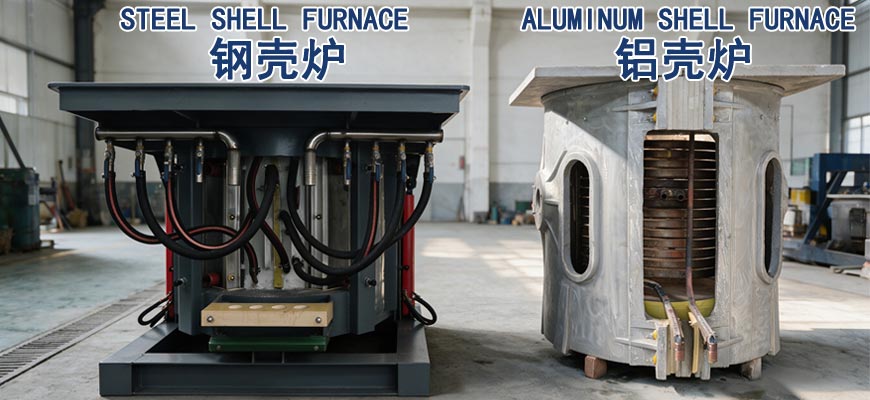
The solution includes steel-shell/aluminum-shell MF melting furnaces, KGPS/IGBT MF power supplies, optional electromagnetic stirring system (for master alloys), and water temperature/pressure monitoring. Furnace lining uses dry-vibrated neutral/basic material, suitable for cast steel, cast iron, high-manganese steel, nickel-based alloys, and scrap steel recycling & remelting in continuous high-temperature operations — providing one-stop service from equipment selection to production handover.
Six Technical Advantages · Purpose-Built for Ferrous Metal High-Temperature Melting
Medium-frequency induction heating converts electrical energy directly into heat — overall power consumption 15%+ below industry average, significantly reducing ferrous metal melting production costs.
High power density design enabling rapid melting across 0.1–20 ton capacities, reducing per-charge cycle time by 25% and significantly boosting cast steel and cast iron throughput.
Freely adjustable temperature range with infrared temperature measurement ±5°C precision + PLC closed-loop control, ensuring stable high-temperature melt — no overheating or under-temperature issues.
Supports remote connection via phone or computer — monitor melting status anytime, anywhere, retrieve historical production records, and check power consumption.
Furnace lining uses dry-vibrated neutral/basic material with temperature resistance up to 1700°C+. Normal lining life exceeds 200 heats, suitable for extended continuous high-temperature operations.
Multiple safety protections: leak detection alarm, water temperature monitoring, over-current/over-voltage protection, emergency stop — equipment service life exceeding 10 years.
Ferrous metals and their alloys (steel, iron, manganese, nickel, etc.) have high melting points, typically 1500–1700°C, demanding exceptional temperature resistance, lining life, and power density. Henan Rongke Electric provides high-power steel-shell medium-frequency melting furnaces with premium dry-vibrated neutral/basic lining for sustained high-temperature continuous operation.
Precision and sand casting of carbon steel, alloy steel, and stainless steel — suitable for valves and construction machinery castings.
Melting of gray iron, ductile iron, and compacted graphite iron — suitable for automotive parts, pipes, and machine tool beds.
Formulation and melting of high-manganese steel, nickel-based superalloys, and chromium-series wear-resistant alloys.
Recycling and purification of scrap steel, steel chips, and iron chips — resource circular utilization to reduce raw material costs.
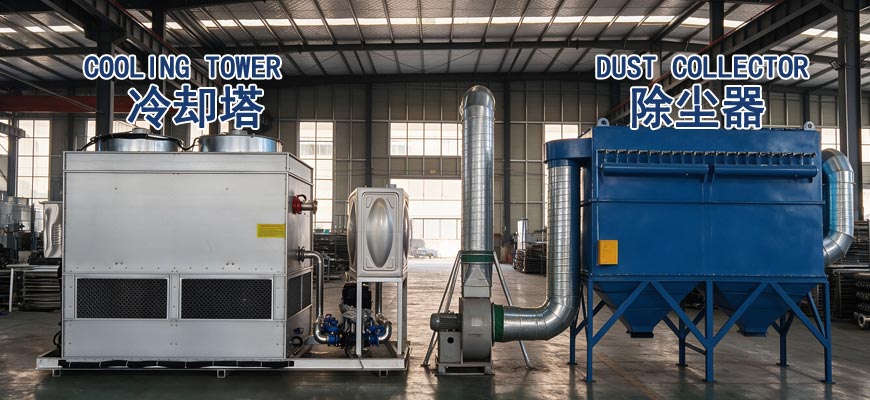
Four Core Equipment Types · Configured for Ferrous Metal High-Temperature Melting


| Model | Power | Applicable Metal | Rated Capacity | Melting Rate | Furnace Shell | Tilting Method |
|---|---|---|---|---|---|---|
| GW-0.15T | Please consult sales | Steel, Iron, Mn, Ni, etc. | 0.15 t | 0.15 t/h | Steel or Aluminum Shell | Hydraulic or Gearbox Tilting |
| GW-0.25T | Please consult sales | Steel, Iron, Mn, Ni, etc. | 0.25 t | 0.25 t/h | Steel or Aluminum Shell | Hydraulic or Gearbox Tilting |
| GW-0.35T | Please consult sales | Steel, Iron, Mn, Ni, etc. | 0.35 t | 0.35 t/h | Steel or Aluminum Shell | Hydraulic or Gearbox Tilting |
| GW-0.5T | Please consult sales | Steel, Iron, Mn, Ni, etc. | 0.5 t | 0.50 t/h | Steel or Aluminum Shell | Hydraulic or Gearbox Tilting |
| GW-0.75T | Please consult sales | Steel, Iron, Mn, Ni, etc. | 0.75 t | 0.75 t/h | Steel or Aluminum Shell | Hydraulic or Gearbox Tilting |
| GW-1T | Please consult sales | Steel, Iron, Mn, Ni, etc. | 1 t | 1.2 t/h | Steel or Aluminum Shell | Hydraulic or Gearbox Tilting |
| GW-1.5T | Please consult sales | Steel, Iron, Mn, Ni, etc. | 1.5 t | 1.8 t/h | Steel or Aluminum Shell | Hydraulic or Gearbox Tilting |
| GW-2T | Please consult sales | Steel, Iron, Mn, Ni, etc. | 2 t | 2.5 t/h | Steel or Aluminum Shell | Hydraulic or Gearbox Tilting |
| GW-3T | Please consult sales | Steel, Iron, Mn, Ni, etc. | 3 t | 3.6 t/h | Steel or Aluminum Shell | Hydraulic or Gearbox Tilting |
| GW-4T | Please consult sales | Steel, Iron, Mn, Ni, etc. | 4 t | 4.5 t/h | Steel or Aluminum Shell | Hydraulic or Gearbox Tilting |
| GW-5T | Please consult sales | Steel, Iron, Mn, Ni, etc. | 5 t | 5.6 t/h | Steel or Aluminum Shell | Hydraulic or Gearbox Tilting |
| GW-8T | Please consult sales | Steel, Iron, Mn, Ni, etc. | 8 t | 9 t/h | Steel or Aluminum Shell | Hydraulic or Gearbox Tilting |
| GW-10T | Please consult sales | Steel, Iron, Mn, Ni, etc. | 10 t | 10 t/h | Steel or Aluminum Shell | Hydraulic or Gearbox Tilting |
| GW-15T | Please consult sales | Steel, Iron, Mn, Ni, etc. | 15 t | 15 t/h | Steel or Aluminum Shell | Hydraulic or Gearbox Tilting |
| GW-20T | Please consult sales | Steel, Iron, Mn, Ni, etc. | 20 t | 20 t/h | Steel or Aluminum Shell | Hydraulic or Gearbox Tilting |
* Above are typical parameters for ferrous metal melting; specific configuration is customized based on alloy grade and capacity requirements.
Whether melting cast steel, cast iron, manganese steel, or nickel-based alloys, whether building a new production line or upgrading equipment, our engineering team will provide a tailored equipment configuration based on your metal type, capacity requirements, and site conditions.